 EN
Navigating Global Compliance in Modern Industrial Packaging Systems and Supply Chains
When scaling international supply chains and expanding manufacturing footprints across cross-border markets, procurement managers, plant directors, and operations leads often encounter a critical regulatory hurdle. Ensuring that every piece of heavy machinery integrated into the production line meets stringent regional safety directives, mechanical standards, and environmental benchmarks is imperative. For modern enterprises investing heavily in a fully automatic shrink packaging machine, verifying regulatory compliance—especially internationally recognized marks—is never merely a bureaucratic formality. Instead, it serves as a vital corporate safeguard protecting operator safety, minimizing legal liability, and facilitating frictionless market entry across European and global economic territories. Navigating these multi-layered compliance requirements demands a comprehensive, deeply technical understanding of global machinery directives, risk assessment methodologies, and standardized conformity assessment procedures that govern contemporary automated factory floors.
Decoding CE Certification: Why It Matters for a Fully Automatic Shrink Packaging Machine
The Conformité Européene (CE) mark functions as an official manufacturer's declaration and legal attestation that a specific industrial product complies entirely with the essential health, safety, protection, and environmental mandates outlined within applicable European Union harmonization directives. For a fully automatic shrink packaging machine, securing official CE certification entails undergoing rigorous, multi-stage conformity assessments closely aligned with foundational regulations such as the European Machinery Directive (2006/42/EC), along with relevant harmonized standards like EN ISO 12100 for machinery risk assessment and reduction. According to international industrial engineering guidelines, certified packaging systems must undergo exhaustive third-party or internal evaluations regarding electrical safety configurations, mechanical risk reduction parameters, pneumatic pressure limits, and electromagnetic compatibility (EMC). This certification officially confirms that the equipment satisfies the highest global benchmarks for operational hazard mitigation, effectively shielding factory operators from thermal burns, pinch points, and moving-part injuries during continuous high-tempo operation.
Engineering Excellence: Core Technical Advantages of Certified Systems
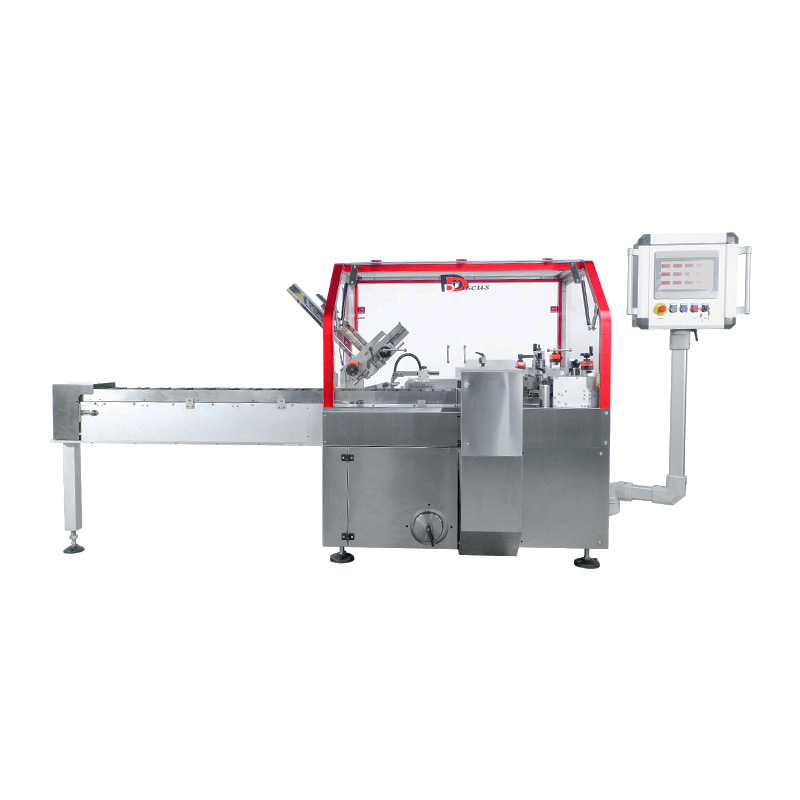
Drawing from extensive, hands-on engineering experience in managing automated secondary packaging lines across diverse manufacturing plants, certified industrial machinery consistently demonstrates superior reliability, structural integrity, and operational uptime under relentless high-speed production schedules. A premium fully automatic shrink packaging machine incorporates advanced programmable logic controllers (PLCs), intuitive human-machine interfaces (HMIs), proportional temperature control loops, and multi-layered emergency stop interlocks engineered strictly to international safety standards. In practical, day-to-day factory applications, these integrated technological safeguards dramatically minimize unexpected downtime triggered by film feeding jams, sealing wire degradation, or thermal overloads. Furthermore, sophisticated photoelectric sensors, automated film tension controllers, and intelligent temperature feedback mechanisms ensure uniform shrink film wrapping and pristine package integrity across diverse product geometries, ultimately slashing raw material waste and maximizing overall equipment effectiveness (OEE) across the entire production facility.
Commercial ROI: How Regulatory Compliance Drives Long-Term Business Value
Beyond satisfying baseline technical specifications and safety codes, achieving verified regulatory compliance translates directly into tangible, long-term commercial advantages for global manufacturing enterprises. Deploying a fully CE-compliant fully automatic shrink packaging machine significantly lowers corporate legal liabilities, mitigates costly customs clearance delays at international ports of entry, and dramatically reduces workplace injury frequencies and associated workers' compensation claims. From a strategic financial perspective, although fully compliant automated systems frequently demand a higher initial capital investment compared to non-certified alternatives, they deliver an exceptionally robust return on investment (ROI). This superior financial return is realized through extended equipment lifespans, drastically reduced routine maintenance frequencies, lower energy consumption profiles, and enhanced retail-ready product presentation that consistently elevates consumer confidence in competitive international retail environments.
Mitigating Supply Chain Risks Through Accredited Manufacturing Partnerships
In today's highly interconnected global trade ecosystem, supply chain disruptions and regulatory crackdowns pose severe threats to ongoing business continuity. Working with equipment suppliers who lack certified quality management frameworks can result in rejected shipments, hefty regulatory fines, and catastrophic operational delays. Conversely, partnering with established manufacturers who rigorously integrate international compliance standards into every production phase ensures complete transparency, traceability, and operational peace of mind. This proactive approach to quality assurance guarantees that every automated packaging unit arriving at your facility is ready for immediate, compliant deployment, thereby fortifying your entire operational infrastructure against unforeseen regulatory shifts and border inspection scrutiny.
Discus: Your Trusted Global Partner for Compliant Packaging Solutions
Navigating the complex landscape of international machinery compliance, safety directives, and custom packaging requirements requires a dedicated manufacturing partner possessing profound industry expertise, advanced engineering capabilities, and robust global supply chain execution. At Discus, we specialize in designing and engineering state-of-the-art packaging and filling solutions meticulously constructed to satisfy rigorous international standards, thereby guaranteeing seamless mechanical and digital integration into your existing production facilities. Backed by extensive manufacturing experience, strict quality control protocols, and an uncompromising commitment to precision craftsmanship, Discus delivers exceptionally reliable, high-performance automated systems tailored specifically to the dynamic, evolving demands of the global cosmetics, food processing, pharmaceutical, and chemical manufacturing industries. Partner with Discus today to elevate your plant production efficiency, safeguard your workforce, and secure an enduring competitive edge in the global marketplace.
Table of Contents
- Navigating Global Compliance in Modern Industrial Packaging Systems and Supply Chains
- Decoding CE Certification: Why It Matters for a Fully Automatic Shrink Packaging Machine
- Engineering Excellence: Core Technical Advantages of Certified Systems
- Commercial ROI: How Regulatory Compliance Drives Long-Term Business Value
- Mitigating Supply Chain Risks Through Accredited Manufacturing Partnerships
- Discus: Your Trusted Global Partner for Compliant Packaging Solutions